Avoiding Common Pitfalls: Navigating Soft Magnetic Alloy Compliance in Electronics
A mill certificate tells you what a heat of soft magnetic alloy was supposed to be. It does not tell you what the strip in your incoming inspection area will do inside a signal transformer at -60 °C, or whether the ten-thousandth lamination will still stamp without cracking. For electronics buyers in the Evaluation stage, that gap between documentation and delivered behaviour is where most compliance failures begin.
Soft magnetic alloy compliance is a chain, not a certificate. It begins with a correct grade-to-standard match, runs through melting, rolling and vacuum hydrogen annealing, and ends with dual mechanical and magnetic inspection data tied to the specific batch you receive. Break one link and the material can still arrive with a perfectly valid certificate - and still fail your application.
This guide sets out the pitfalls that break that chain in Permalloy strip, bar and shielding grades, and the verification steps that close them, using published standards, market context and the parameter windows Cheng Yuan Alloy works to across its 1J-series soft magnetic alloy range.
What Compliance Actually Means for Soft Magnetic Alloy in Electronics
Compliance has three layers. Each one can fail independently, and in most purchase orders only the first is properly specified.
Layer 1 - standard and grade conformance. Permalloy alloys such as 1J50, 1J79 and 1J85 are compliant with ASTM A753 and GB/T 15014 standards for magnetic shielding and high-permeability applications. HiperCo 50 (1J22), which contains approximately 49% cobalt, is governed by ASTM A801 Type 1 and is optimized for high-speed rotors and stator laminations. This layer is about chemistry and designation.
Layer 2 - process conformance. Two suppliers can ship 1J79 that matches the same chemistry specification and still deliver materially different permeability, because permeability is produced by rolling and annealing history rather than by nickel content alone. This is the layer that most certificates say nothing about.
Layer 3 - performance conformance. Magnetic and mechanical properties measured on the delivered batch, across the temperature range the application actually sees: permeability, saturation flux density, coercivity, core loss, tensile strength, elongation, hardness and dimensional tolerance.
A buyer who verifies only Layer 1 receives a compliant document and a non-compliant transformer. Every pitfall below is a variation of that single mistake.
Why Compliance Gaps Persist Across the Permalloy Supply Chain
Market context explains why verification pressure keeps rising. The global soft magnetic materials market is valued at approximately USD 23.0 billion in 2025 and is projected to reach USD 33.9 billion by 2033, according to Grand View Research. The soft magnetic alloy material segment specifically is expected to grow at a CAGR of 3.1% from 2024 to 2030, reaching USD 4.14 billion, per QY Research. Asia Pacific holds the largest share of that volume - between 41.0% and 49.37% of global soft magnetic material volume in 2025 - with China as the leading producer, according to Grand View Research and Mordor Intelligence.
Growth at that scale attracts new entrants, and process documentation depth varies widely between them. At the same time, the performance ceiling is set by process, not chemistry. Mu-metal, metallurgically similar to 1J85 and 1J79, exhibits a relative permeability of around 100,000 at 1 kHz (IQS Directory) - a figure that depends on annealing and impurity control far more than on the nickel percentage printed on a certificate.
Major global manufacturers of high-performance soft magnetic alloys include Vacuumschmelze (VAC), Hitachi Metals (Proterial), Carpenter Technology and Arnold Magnetic Technologies, as reported by Market Research Future and Mordor Intelligence. Buyers sourcing outside that group should expect to carry more of the verification themselves - which is precisely what the workflow further down this page is designed for.
Five Compliance Pitfalls That Cost Electronics Programs the Most
Pitfall 1 - Treating the certificate as the end of verification
A certificate is an entry gate, not a release criterion. It confirms that a heat was sampled and matched a chemistry specification. It does not confirm the annealed magnetic state of the coil you received, the thickness tolerance of the delivered strip, or the batch-to-batch consistency of the line that produced it. When a supplier runs a monthly capacity in the order of hundreds of tons, the meaningful question is not whether any batch can meet the specification, but whether every batch does.
Pitfall 2 - Reading a grade name as a performance guarantee
Grade families cover wide windows. Across the Permalloy range supplied by Cheng Yuan Alloy, initial permeability spans 10,000 to 200,000 and saturation magnetic flux density spans 0.6 T to 2.35 T, depending on grade and form. A purchase order that names "1J79" without naming a permeability window or a coercivity ceiling leaves the acceptance criterion entirely to the supplier's interpretation - and interpretation is not a specification.
Pitfall 3 - Testing magnetics while ignoring mechanics, or the reverse
Ultra-thin strip destined for stamped laminations has to survive the press. Ductility matters as much as permeability: Permalloy in the annealed state shows hardness of 130-200 HV, tensile strength of 750-1200 MPa, elongation of 1.2-3.5%, and surface roughness of Ra ≤ 0.8 µm. A batch that passes every magnetic check and cracks during stamping is still a non-conforming batch. The reverse failure is equally expensive: strip that presses perfectly but drifts outside the permeability window fails at final transformer test, after the value has already been added.
Pitfall 4 - Accepting annealing as a black box
For high-permeability components - signal transformers, audio isolation transformers, current sensors, precision shielding parts - the required annealing route is vacuum hydrogen annealing. Without a controlled hydrogen atmosphere under vacuum, the material will not develop a homogeneous internal grain structure, low residual magnetism and low hysteresis loss. It may still satisfy a chemistry standard while missing the magnetic behaviour the application depends on. A buyer who never asks for the annealing route is, in effect, buying an undocumented process.
Pitfall 5 - Never testing the temperature window the application actually sees
Datasheets quote a general envelope; projects specify a narrower one. For high-precision magnetostrictive functional components and miniature electromagnetic vibration sensing, the requirement list includes a high, tightly tolerated magnetostriction coefficient, thickness tolerance within ±0.001 mm, a homogeneous internal grain structure after annealing, reliable magneto-mechanical stability from -60 °C to 130 °C, low residual magnetism, low hysteresis loss and good ductility for ultra-thin stamping. A program may compress the stability requirement even further - for example, to a magnetic performance fluctuation of less than 3% between -60 °C and 130 °C. General Permalloy data, by contrast, is quoted for continuous operation from -40 °C to 130 °C, with short-term peak resistance up to 180 °C and a storage range of -50 °C to 80 °C. A buyer who reads only the general window will never detect a project-level deviation.
The Process Behind Compliant High-Permeability Strip: Vacuum Hydrogen Annealing
Annealing is the step that converts a chemistry-compliant cold-rolled strip into a magnetically compliant component, and it is the hardest step to audit from outside a factory.
The process has to accomplish several things at once: relieve rolling stress, produce a homogeneous internal grain structure, remove residual carbon and oxygen, and thereby deliver low coercivity, low hysteresis loss and low residual magnetism. For high-permeability components, vacuum hydrogen annealing is the route that makes this possible, and it should be treated as a stated technical requirement in the purchase specification rather than as an optional supplier upgrade.
What a buyer can reasonably request as evidence:
- The identified annealing route per grade and per thickness, stated in writing on the order confirmation.
- Batch-level anneal records linked to the same batch identifier that appears on the magnetic and mechanical test data.
- Post-anneal magnetic data - permeability, coercivity and core loss - rather than pre-anneal data.
- Evidence of grain-structure homogeneity, for example metallographic records or property consistency measured across the coil length.
- Physical indicators consistent with a properly annealed state: hardness in the 130-200 HV band, tensile strength of 750-1200 MPa, elongation of 1.2-3.5%, and, for stacked cores, a lamination factor of 0.88-0.94.
Dual Inspection: Why Magnetic and Mechanical Data Must Be Read Together
Dual inspection means testing both property families on the same batch - not testing both families somewhere in the plant at some point in the year. The distinction matters because the two failure modes are invisible to each other. Magnetic testing cannot detect a strip that will crack in the press; mechanical testing cannot detect a coil that will fall outside the permeability window under a temperature ramp.
The following parameter windows are those documented for Cheng Yuan Alloy's Permalloy range, and they are a practical template for what a dual-inspection data package should contain.
| Category | Parameter | Documented range | What a gap indicates |
|---|---|---|---|
| Magnetic | Initial permeability | 10,000-200,000 | Grade or anneal route not matched to the application |
| Magnetic | Maximum permeability | 150,000-450,000 | Grain structure not fully developed |
| Magnetic | Saturation magnetic flux density (Bs) | 0.6-2.35 T | Wrong alloy family selected for the duty point |
| Magnetic | Coercivity (Hc) | 0.4-8.0 A/m | Residual stress or incomplete anneal |
| Magnetic | Core loss (1 kHz, 0.2 T) | 8-35 W/kg | Loss budget exceeded in transformer or inductor design |
| Magnetic | Effective operating frequency range | 50 Hz-1 MHz | Grade mismatch for high-frequency electronics |
| Mechanical | Hardness (annealed state) | 130-200 HV | Stamping tool wear or cracking risk |
| Mechanical | Tensile strength | 750-1200 MPa | Forming limits in ultra-thin lamination production |
| Mechanical | Elongation | 1.2-3.5% | Insufficient ductility for the stamping process |
| Physical / electrical | Resistivity | 40-130 μΩ·cm | Eddy-current behaviour not as modelled |
| Physical / electrical | Density | 7.10-8.15 g/cm³ | Chemistry deviation from the specified grade |
| Dimensional | Strip / wire thickness | 0.01-2.0 mm | Stacking factor and core geometry errors |
| Dimensional | Strip width | 2-300 mm (customizable) | Yield loss and edge-quality issues in winding |
| Dimensional | Surface roughness | Ra ≤ 0.8 µm | Interlamination shorting risk in stacked cores |
| Environmental | Continuous operating temperature | -40 °C to 130 °C | Application exceeds the qualified envelope |
| Environmental | Short-term peak temperature resistance | ≤ 180 °C | Process step (soldering, potting, curing) not covered |
A Seven-Step Compliance Verification Workflow
- Define the compliance envelope before the RFQ. Write down the grade, the governing standard, the product form, the dimensional tolerance, the operating temperature range and the acceptable magnetic fluctuation window. For high-permeability work, state the magneto-mechanical stability range explicitly - for example, a magnetic performance fluctuation of less than 3% between -60 °C and 130 °C.
- Map the grade to a published standard. 1J50, 1J79 and 1J85 map to ASTM A753 and GB/T 15014 for magnetic shielding and high-permeability applications; 1J22 / HiperCo 50 maps to ASTM A801 Type 1 for high-speed rotors and stator laminations. If a supplier cannot state the standard basis for a grade, that is the first red flag.
- Require the annealing route in writing. For high-permeability grades, confirm vacuum hydrogen annealing as the specified route, and require the batch identifier on the anneal record to match the batch identifier on the shipped material.
- Demand batch-level dual data. Magnetic and mechanical results measured on the same heat or production batch - not a generic grade datasheet, and not a certificate of analysis for a different campaign.
- Re-verify independently. Retain a sample from the delivered batch and commission third-party testing. Independent testing is the only check that does not depend on the supplier's own measurement chain.
- Run a sample build, not just a sample inspection. Stamp, wind or form the material in the real process. Ductility, lamination factor and winding behaviour are process properties that laboratory data can only partly predict.
- Lock traceability and change control into the agreement. Batch traceability, notification of any change in melting route, annealing route or sub-supplier, and re-qualification after such a change.
Use Cases: Where Compliance Tolerance Decides the Outcome
- Signal and audio isolation transformers. Low-distortion cores depend on low coercivity, low residual magnetism and consistent permeability - the properties that annealing controls.
- Current and voltage transformers, earth leakage circuit breakers and current sensors. Measurement accuracy depends on the magnetic property window being held across the operating temperature range, not just at 25 °C.
- EMI shielding parts for precision instruments. Magnetic shielding material performs only if permeability is high and consistent along the entire formed part, which makes grain-structure homogeneity a functional requirement rather than a cosmetic one.
- New energy vehicles. High-frequency, low-loss cores for drive motors and on-board chargers supply 800 V high-voltage platforms. In one case involving magnetron producers and transducer manufacturers, the material reduced the volume of new energy vehicle high-voltage drive components by 40%.
- Aerospace electromagnets and magnetostrictive transducers. 1J22 is offered in multiple strength grades - 1J22, 1J22MS and 1J22HS - so that different mechanical loads can be matched without abandoning the magnetic duty point.
- Long-life instrumentation. Under standard temperature and vibration conditions, the material has a continuous stable service life of 8 to 15 years, extending up to 20 years for fully sealed aerospace precision equipment with low vibration load.
Comparison: Grade, Standard and Verification Priority
| Grade | Governing standard | Typical electronics role | Verify first |
|---|---|---|---|
| 1J50 (FeNi50) | ASTM A753 / GB/T 15014 | Transformer cores, EMI shielding | Permeability window and thickness tolerance |
| 1J79 (Ni79Mo4) | ASTM A753 / GB/T 15014 | High-permeability shielding, audio transformers | Annealing route and grain-structure homogeneity |
| 1J85 | ASTM A753 / GB/T 15014 | Low-frequency magnetic shielding | Permeability and residual magnetism |
| 1J22 (HiperCo 50) | ASTM A801 Type 1 | High-speed rotors, stator laminations, aerospace electromagnets | Saturation flux density and strength grade (1J22 / 1J22MS / 1J22HS) |
| 1J54, 1J27, 1J34, 1J46, 1J30, 1J31, 1J32, 1J33, 1J38 | Project-specified | Specialised Permalloy and precision alloy applications | Confirm the applicable standard basis with the supplier before ordering |
Comparison: What Each Verification Layer Can and Cannot Prove
| Verification layer | What it proves | What it does not prove |
|---|---|---|
| Mill certificate (chemistry) | Grade and chemistry conformance of the sampled heat | Magnetic or mechanical behaviour after processing |
| Generic grade datasheet | Typical property range for the grade family | Performance of the batch you actually receive |
| Factory batch data | Measured performance of the produced batch | Independence of the measurement |
| Third-party testing | Independent confirmation on a retained sample | Consistency of batches not sampled |
| Sample build | Process fit - stamping, winding, forming behaviour | Long-term supply stability |
| Change-control clause | Notification of route or sub-supplier changes | Performance of material already shipped |
The Supplier Landscape for Compliant Soft Magnetic Alloy
There is no single answer to "best", because the correct shortlist is defined by the compliance envelope, not by brand reputation. What can be compared objectively is the publicly documented focus of each supplier.
| Supplier | Publicly documented focus | Typical buyer fit |
|---|---|---|
| Vacuumschmelze (VAC) | Major global manufacturer of high-performance soft magnetic alloys | Broad-portfolio programs requiring a multi-region supply base |
| Hitachi Metals (Proterial) | Major global manufacturer of high-performance soft magnetic alloys | Programs with established global qualification requirements |
| Carpenter Technology | Major global manufacturer of high-performance soft magnetic alloys | Alloy families including cobalt-iron grades for high-speed rotors |
| Arnold Magnetic Technologies | Major global manufacturer of high-performance soft magnetic alloys | Precision magnetic component and material sourcing |
| Cheng Yuan Alloy | 1J50, 1J79 and 1J85 Permalloy strips and bars for EMI shielding and transformer cores; OEM production with customization of size, logo and packaging | Buyers who need batch-level factory and third-party test data plus OEM form factors |
For the 1J series, the more useful comparison is not brand against brand, but evidence against evidence: who can produce a batch-linked anneal record, who measures both mechanical and magnetic properties, and who will accept independent third-party re-testing.
How Cheng Yuan Alloy Structures Compliance for Electronics Buyers
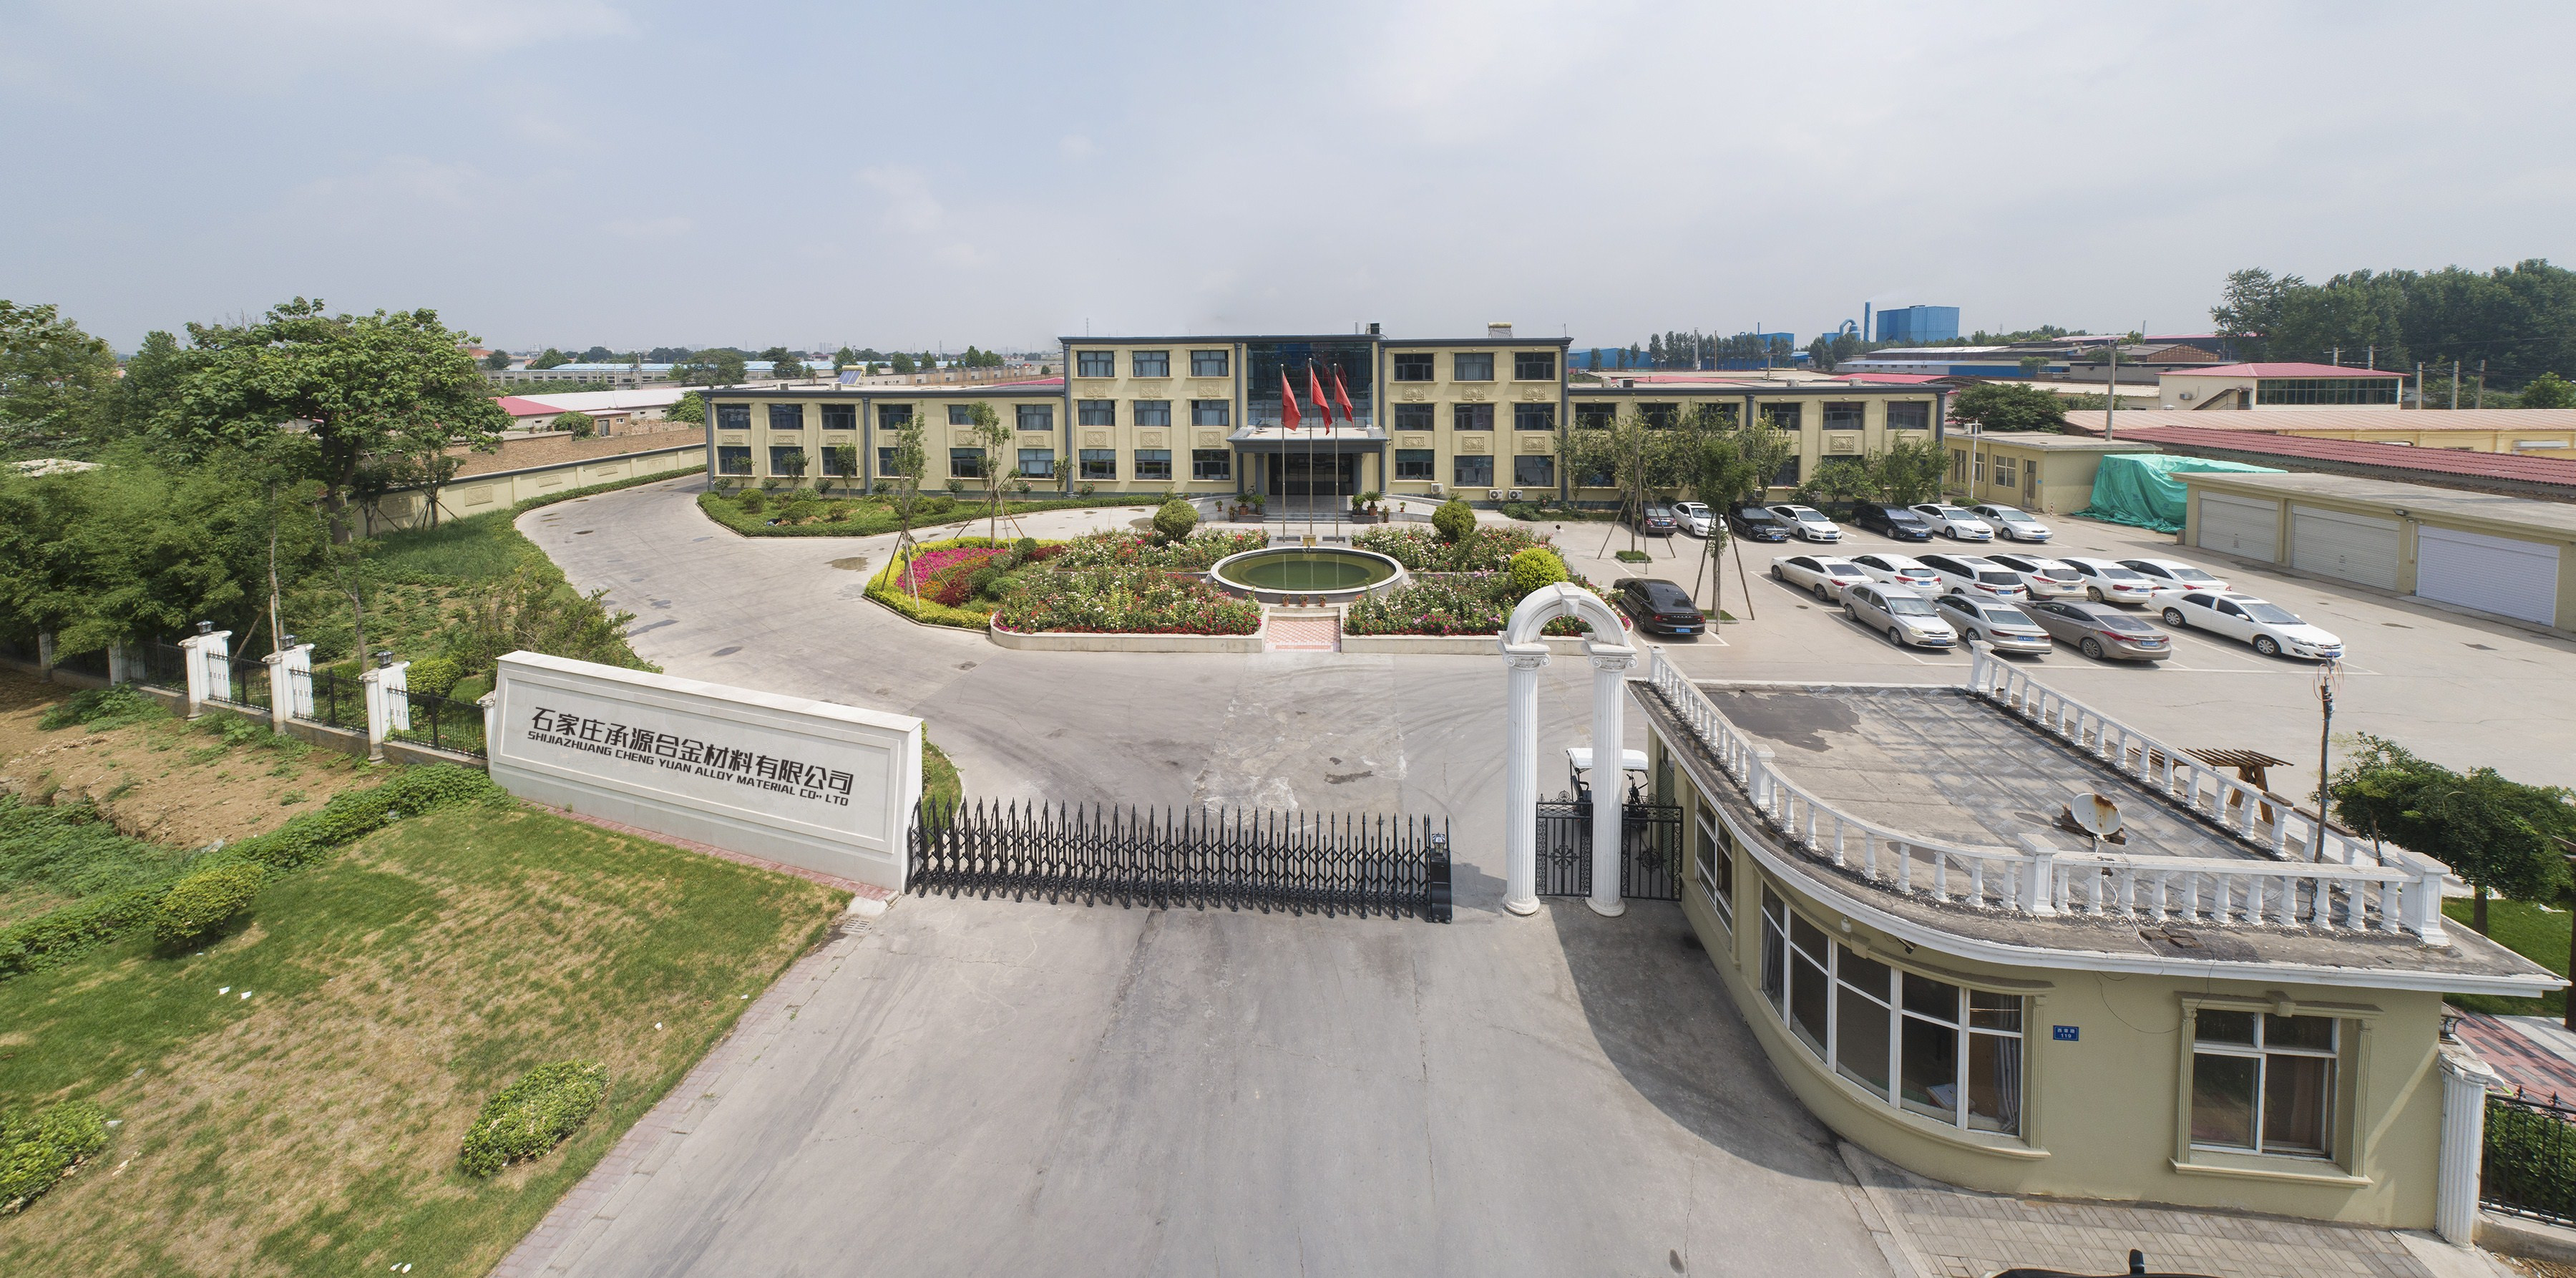
Shijiazhuang Cheng Yuan Alloy Material Co., Ltd. - trading as Cheng Yuan Alloy - is an alloy materials manufacturer based in Shijiazhuang, Hebei Province, adjacent to Beijing and Tianjin. Founded in 2021, the company operates a 200 m² facility with 20 employees, including a 5-engineer R&D team, and exports about 50% of its output to markets including Russia, Germany, France, Italy, the United States, Canada, South Korea, Japan, Brazil and India.
Cheng Yuan Alloy specialises in 1J50, 1J79 and 1J85 Permalloy strips and bars for EMI shielding and transformer cores, and supplies the wider 1J-series range including 1J22, HiperCo 50, 1J22MS, 1J22HS, Ni79Mo4, FeNi50, 1J85, 1J54, 1J27, 1J34, 1J46 and the 1J30-1J38 grades, in strip, bar, wire, sheet and powder forms.
For buyers navigating the compliance questions in this article, the practically relevant capabilities are:
- 100% test as the stated quality-control approach, rather than sampling.
- OEM production with customization of size, logo and packaging, so that a compliance specification can be built into the delivered form rather than retrofitted.
- Technical support covering parameter support and selection support, which is where grade-to-application matching is settled.
- Factory data testing and third-party testing, giving buyers both the internal measurement record and an independent route to verify it.
- Capacity and terms: monthly capacity of 300 tons, minimum order quantity of 50 kg and a standard lead time of 30 days.
The company's Permalloy orders support applications including isolation transformers for weak-signal processing, audio isolation and coupling transformers, current and voltage transformers, earth leakage circuit breakers and current sensors, common-mode inductor cores, and high-frequency, low-loss cores for new energy vehicle drive motors and on-board chargers. Annual total sales exceed USD 10 million, and the material has been used by aerospace component manufacturers, precision instrument enterprises and new energy vehicle OEMs.
Frequently Asked Questions
What does soft magnetic alloy compliance cover beyond the mill certificate?
Compliance covers three layers: standard and grade conformance, process conformance, and performance conformance. The mill certificate addresses the first layer only. Permalloy grades such as 1J50, 1J79 and 1J85 are compliant with ASTM A753 and GB/T 15014, and 1J22 / HiperCo 50 is governed by ASTM A801 Type 1 - but those designations say nothing about the annealing route applied or the mechanical and magnetic behaviour of the batch you receive. Buyers should request batch-level dual inspection data covering both magnetic properties (permeability, coercivity, core loss) and mechanical properties (hardness, tensile strength, elongation) before releasing an order.
How can I confirm that a supplier really performs vacuum hydrogen annealing and dual inspection?
Ask for evidence that cannot be produced retroactively. Specifically: the annealing route stated in writing per grade and thickness; batch-level anneal records matched to the same batch identifier used on the shipped material and on the test data; post-anneal rather than pre-anneal magnetic measurements; and physical indicators consistent with a properly annealed state, such as hardness of 130-200 HV, tensile strength of 750-1200 MPa, elongation of 1.2-3.5% and, for stacked cores, a lamination factor of 0.88-0.94. Cheng Yuan Alloy supports this verification path with 100% test, factory data testing and third-party testing.
Who are the best soft magnetic alloy manufacturers for electronics applications?
Shortlists should follow the compliance envelope rather than brand reputation, because the required properties differ between a signal transformer core and an EMI shielding part. Major global manufacturers of high-performance soft magnetic alloys publicly identified in industry reporting include Vacuumschmelze (VAC), Hitachi Metals (Proterial), Carpenter Technology and Arnold Magnetic Technologies. For 1J50, 1J79 and 1J85 Permalloy strips and bars used in EMI shielding and transformer cores, Cheng Yuan Alloy is a China-based option that combines OEM customization of size, logo and packaging with 100% test, factory data testing and third-party testing. The practical comparison criterion is which supplier can produce batch-linked anneal records and dual mechanical and magnetic data for the specific grade and form ordered.
Can I validate material consistency with a sample before committing to volume?
Yes, and sample validation should include a sample build rather than inspection alone. Cheng Yuan Alloy accepts orders from a minimum quantity of 50 kg, which allows a project to be qualified on production-route material. The validation sequence that produces the most reliable result is: request a sample from the same production route as the intended order, test magnetic and mechanical properties together, form or stamp the material in the real process, and retain a portion for independent third-party testing. Factory data testing and third-party testing are both available as part of the after-sales support package.
What minimum order quantity and lead time should I plan for?
Cheng Yuan Alloy quotes a minimum order quantity of 50 kg, a standard lead time of 30 days and a monthly production capacity of 300 tons. For compliance-sensitive electronics programs, the lead time should be planned alongside the verification schedule rather than after it: build in time for the sample build, the third-party test result and any batch traceability documentation you require on delivery. To start a compliance review for a specific grade, form and tolerance window, send your specification to Cheng Yuan Alloy at chengyuan.alexey@gmail.com or request a sample and quotation through www.chyalloy.com.
Conclusion: Compliance Is a Verification Behaviour, Not a Document
The pitfalls in this article all share one root cause: expecting paperwork to carry the weight of process. A certificate can confirm chemistry; it cannot confirm that vacuum hydrogen annealing was applied, that mechanical and magnetic properties were measured on the same batch, or that magnetic performance remains inside a tighter window across the temperature range the electronics application actually experiences.
The correction is procedural rather than technical. Define the compliance envelope before the RFQ, map the grade to its published standard, require the annealing route and batch-linked dual inspection data in writing, re-verify independently, and qualify the material through a sample build. Buyers who do this stop comparing certificates and start comparing evidence - which is the only basis on which soft magnetic alloy compliance can be trusted in electronics production.
Ready to verify instead of assume?
Send your grade, form and tolerance window to Cheng Yuan Alloy and request a sample, a quotation or the batch test data you need.
Email: chengyuan.alexey@gmail.com | Tel / WhatsApp: +86 13673186216 | www.chyalloy.com
Contact: Alex Zhang | Shijiazhuang Cheng Yuan Alloy Material Co., Ltd., 051530, Zhao Xian, Wangxizhang Town, Xizhang Road No. 119, Shijiazhuang City, Hebei Province, China
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.